










Product Details
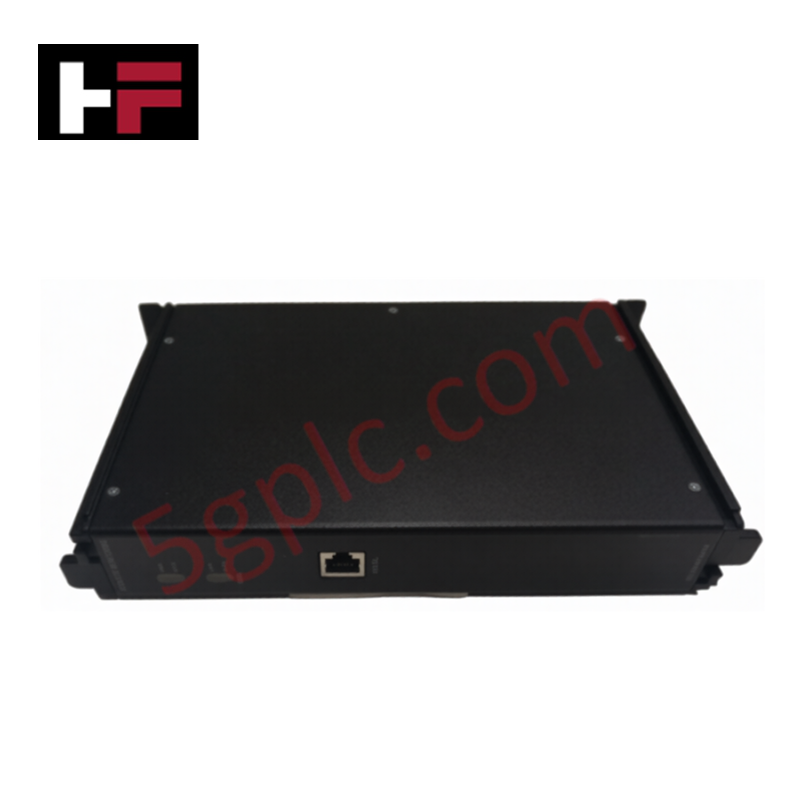
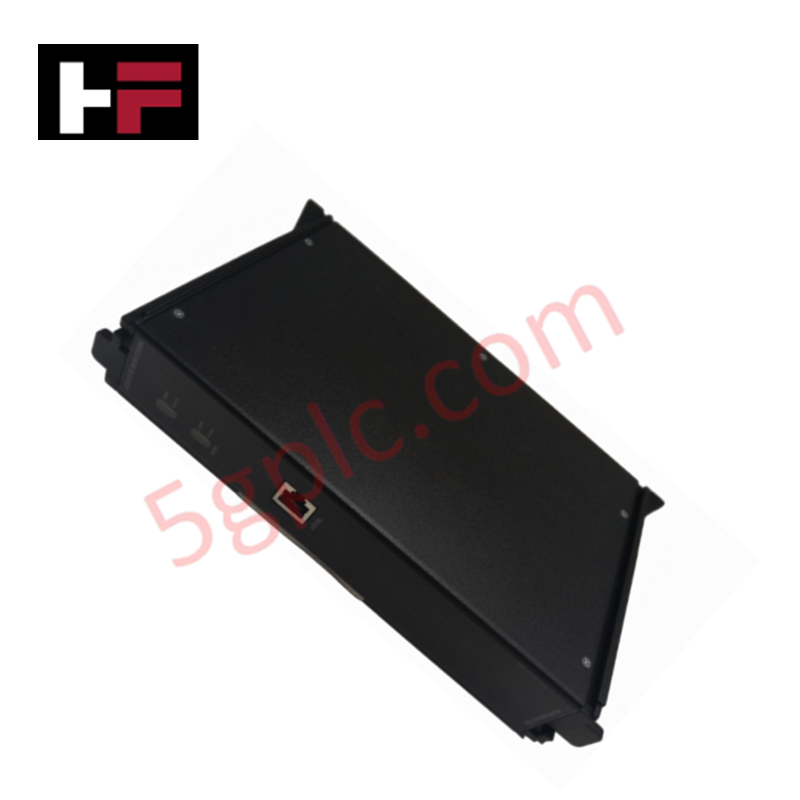
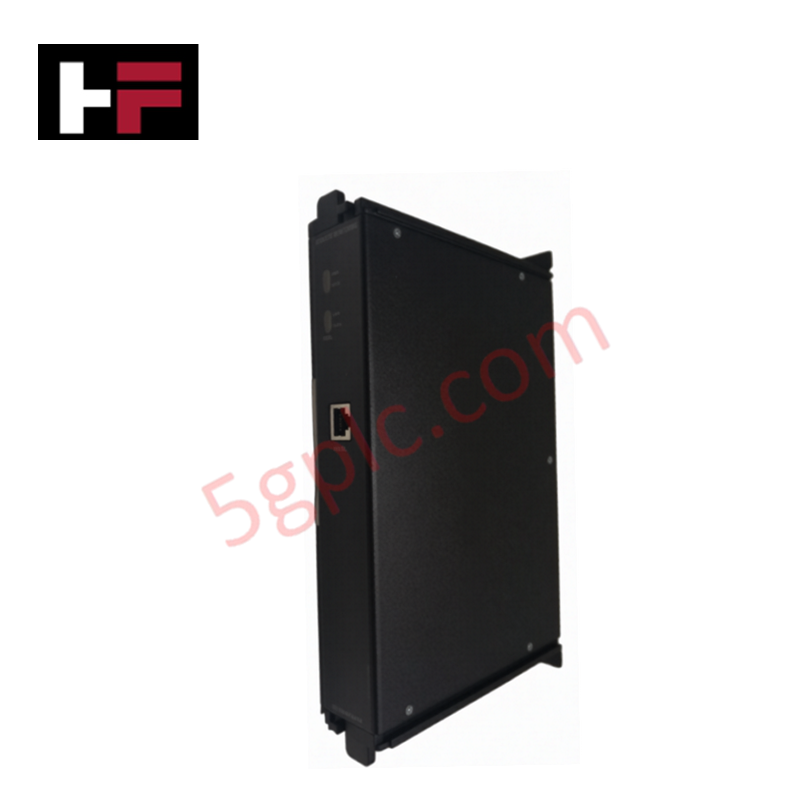
Configured for precision signal regulation in Mark VI platforms, the GE IS210BAPAH1A (IS210BAPAH1A Analog Processor Module) provides direct physical/electrical execution of sensor interfacing and analog signal conditioning for turbine control loops.
Hardware Specifications
| Parameter | Specification |
|---|---|
| Model | IS210BAPAH1A |
| Brand | General Electric |
| Origin | USA |
| Weight | Not specified |
| Dimensions | 23.495 cm x 10.795 cm |
| Operating Temp | -30 deg C to +65 deg C |
| Power Consumption | Not specified |
| Input Voltage | 125 V DC |
| Output Voltage | 24 V DC |
| Mounting | DIN-rail |
Backplane Bus Communication Velocity and Firmware Compatibility
The IS210BAPAH1A operates as a safety I/O pack within the Mark VI control architecture, managing the acquisition of continuous analog inputs from turbine sensors. The module performs real-time signal conditioning—including amplification, filtering, and scaling—to convert raw sensor data into process variables suitable for control logic. Firmware flash compatibility is managed via the controller backplane, ensuring that scaling parameters are synchronized with the master processor's scan cycle. The I/O density scaling supported by this module allows for precise monitoring of temperature, pressure, speed, and fuel flow, maintaining deterministic data throughput across the system bus.
Frequently Asked Questions
Q: Is the IS210BAPAH1A module hot-swappable during turbine operation?
A: Hot-swapping is restricted. The module's integration into active control loops means that removal while the rack is energized will result in a loss of sensor input data, which will trigger a controller fault and potentially a system-level trip.
Q: How is the signal conditioning performed within the module?
A: Raw signals from sensors are routed through internal operational amplifiers and active filter circuits. These components perform signal scaling and noise rejection before the processed data is digitized for transmission across the backplane to the main turbine controller.
Field Installation Guidelines
- Mounting Stability: Install the module on a grounded DIN-rail. Ensure the rail provides a low-impedance path to the cabinet chassis to prevent the accumulation of electrical noise on the analog signal commons.
- Signal Wiring: All analog sensor inputs must be routed using shielded twisted-pair cabling. Terminate cable shields at the designated ground terminals to mitigate the effects of electromagnetic interference on high-impedance input circuits.
- Power Requirements: Ensure the input supply remains stable at 125 V DC. Variations outside the nominal range can result in output voltage instability on the 24 V DC supply side, which may affect the accuracy of external sensor excitation.
- Thermal Considerations: Given the operating range of -30 deg C to +65 deg C, ensure adequate ventilation within the cabinet. Avoid positioning the module adjacent to high-heat sources to prevent thermal drift of the analog components, which could compromise measurement accuracy.
Additional Information
- 100% Genuine Parts: All products are original and authentic, ensuring reliable industrial performance.
- 30-Day Refund Guarantee: Return any in-stock item within 30 days in original, unopened packaging for a full refund (excluding shipping and fees).
- 12-Month Warranty: Covers defects in materials or workmanship; excludes misuse, normal wear, or unauthorized modifications.
- Worldwide Shipping: We ship via USPS, UPS, FedEx, and DHL. Delivery times vary by country and may be subject to customs or import fees.
- Support & Contact: Technical and warranty assistance is available anytime. Contact us here: Contact.
- Purchase Guidance: Check product specifications and compatibility carefully before ordering to ensure proper application.


Tech & Buying Guide

Understanding VFD Mechanical Brake Logic and Control in Industrial Automation
Variable Frequency Drives (VFDs) play a crucial role in modern industrial automation by controlling motor speed, torque, and acceleration. However, high-inertia loads and vertical lifting systems require precise mechanical braking logic to ensure operational safety and prevent equipment damage.

Why Programmable Logic Controllers Drop into Stop Mode: An Expert Analysis
Industrial automation systems rely heavily on Programmable Logic Controllers (PLCs) to maintain uninterrupted production. When a PLC unexpectedly shifts from Run to Stop mode, whole manufacturing lines stall.
As control systems evolve across modern factory automation, understanding the root causes of these interruptions helps engineers minimize costly downtime. This technical guide breaks down why PLCs trip into Stop mode and provides practical strategies to mitigate system faults.

Understanding Root Causes of Unplanned PLC Stop Mode in Industrial Automation
Modern Programmable Logic Controllers manage execution through distinct operational states: Run, Stop, Start-Up, and Hold. During power-up, a controller initializes memory registers within Stop mode before briefly transitioning to Start-Up mode. During this phase, internal self-diagnostics evaluate system integrity across hardware and user programs. If the controller detects no critical faults, it enters Run mode to execute the control program continuously. However, any severe system anomaly forces the CPU back into Stop mode immediately to prevent erratic machine behavior across the plant floor.