












Product Details
Overview:
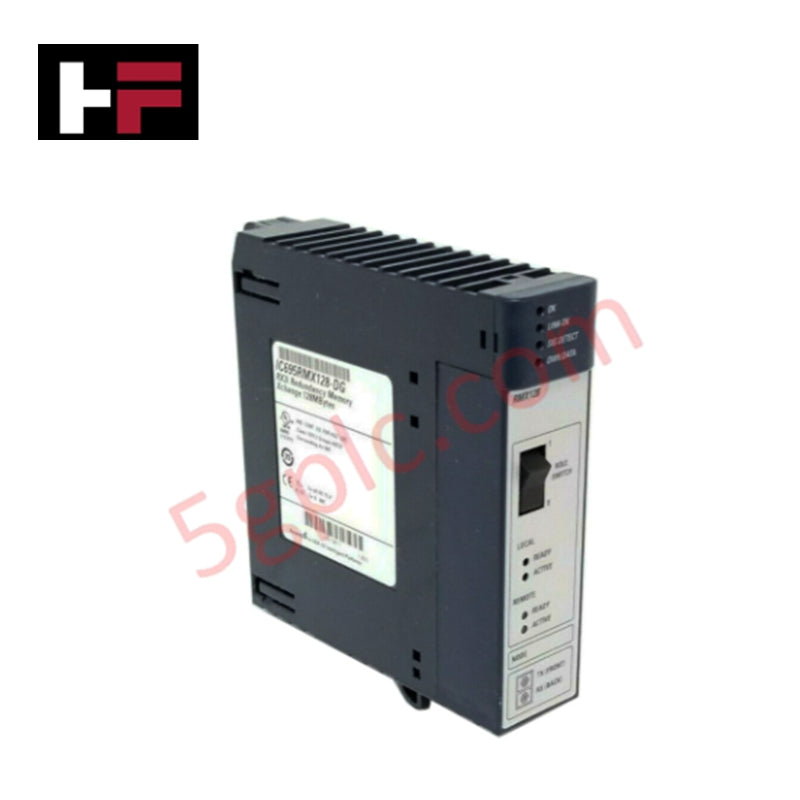
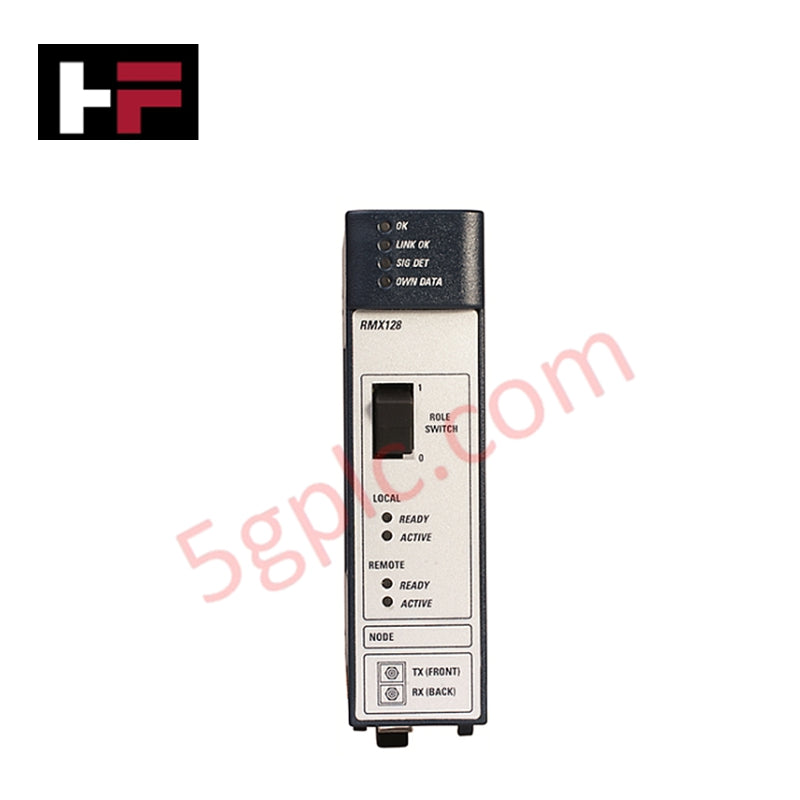
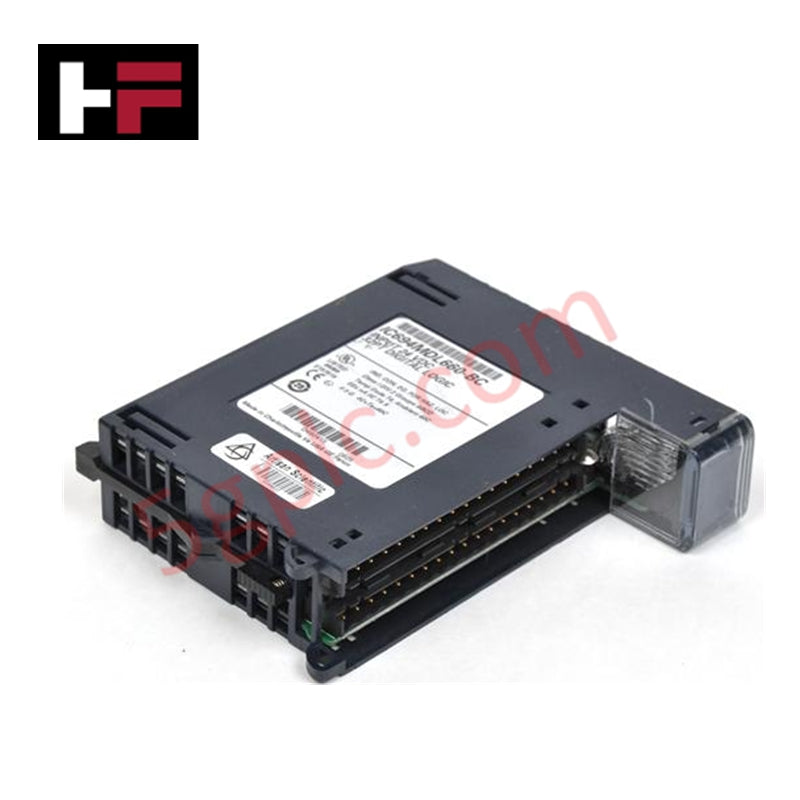
The IC695RMX128 is a high-performance Redundant Memory Xchange (RMX) module from GE Fanuc’s RX3i series. Designed for critical systems, it provides 128 MB of shared memory to enable high-availability data synchronization between redundant controllers. It ensures seamless communication, reduces downtime, and supports robust error detection.
Key Features:
-
Manufacturer: GE Fanuc
-
Model: IC695RMX128
-
Product Type: RX3i Redundant Memory Xchange Module
-
Memory Capacity: 128 Megabytes user-shared memory
-
Module Function: High-availability data synchronization link
-
Backplane Support: Universal backplane using PCI bus
-
Sync Link Speed: 2.1 Gbits/s
-
Communication Data Rate: 2.12 Gbaud
-
Bus Diagnostics: Network error detection for enhanced reliability
-
Redundant RMX Support: Yes, enables controller redundancy
-
Max Distance Between Controllers: 300 meters
-
Slots Required: 1
Applications:
-
Redundant Control Systems: Ideal for mission-critical RX3i PLC setups
-
High Availability Data: Ensures shared memory synchronization between redundant CPUs
-
Industrial Automation: Used in systems requiring maximum uptime and error detection
FAQ:
-
Q: How much shared memory does this module provide?
A: 128 MB for user data and program synchronization. -
Q: Can this module support controller redundancy?
A: Yes, it allows seamless RMX support between two controllers. -
Q: What is the maximum distance between redundant controllers?
A: Up to 300 meters using standard backplane connectivity.
Additional Information
- 100% Genuine Parts: All products are original and authentic, ensuring reliable industrial performance.
- 30-Day Refund Guarantee: Return any in-stock item within 30 days in original, unopened packaging for a full refund (excluding shipping and fees).
- 12-Month Warranty: Covers defects in materials or workmanship; excludes misuse, normal wear, or unauthorized modifications.
- Worldwide Shipping: We ship via USPS, UPS, FedEx, and DHL. Delivery times vary by country and may be subject to customs or import fees.
- Support & Contact: Technical and warranty assistance is available anytime. Contact us here: Contact.
- Purchase Guidance: Check product specifications and compatibility carefully before ordering to ensure proper application.





Tech & Buying Guide

Understanding VFD Mechanical Brake Logic and Control in Industrial Automation
Variable Frequency Drives (VFDs) play a crucial role in modern industrial automation by controlling motor speed, torque, and acceleration. However, high-inertia loads and vertical lifting systems require precise mechanical braking logic to ensure operational safety and prevent equipment damage.

Why Programmable Logic Controllers Drop into Stop Mode: An Expert Analysis
Industrial automation systems rely heavily on Programmable Logic Controllers (PLCs) to maintain uninterrupted production. When a PLC unexpectedly shifts from Run to Stop mode, whole manufacturing lines stall.
As control systems evolve across modern factory automation, understanding the root causes of these interruptions helps engineers minimize costly downtime. This technical guide breaks down why PLCs trip into Stop mode and provides practical strategies to mitigate system faults.

Understanding Root Causes of Unplanned PLC Stop Mode in Industrial Automation
Modern Programmable Logic Controllers manage execution through distinct operational states: Run, Stop, Start-Up, and Hold. During power-up, a controller initializes memory registers within Stop mode before briefly transitioning to Start-Up mode. During this phase, internal self-diagnostics evaluate system integrity across hardware and user programs. If the controller detects no critical faults, it enters Run mode to execute the control program continuously. However, any severe system anomaly forces the CPU back into Stop mode immediately to prevent erratic machine behavior across the plant floor.