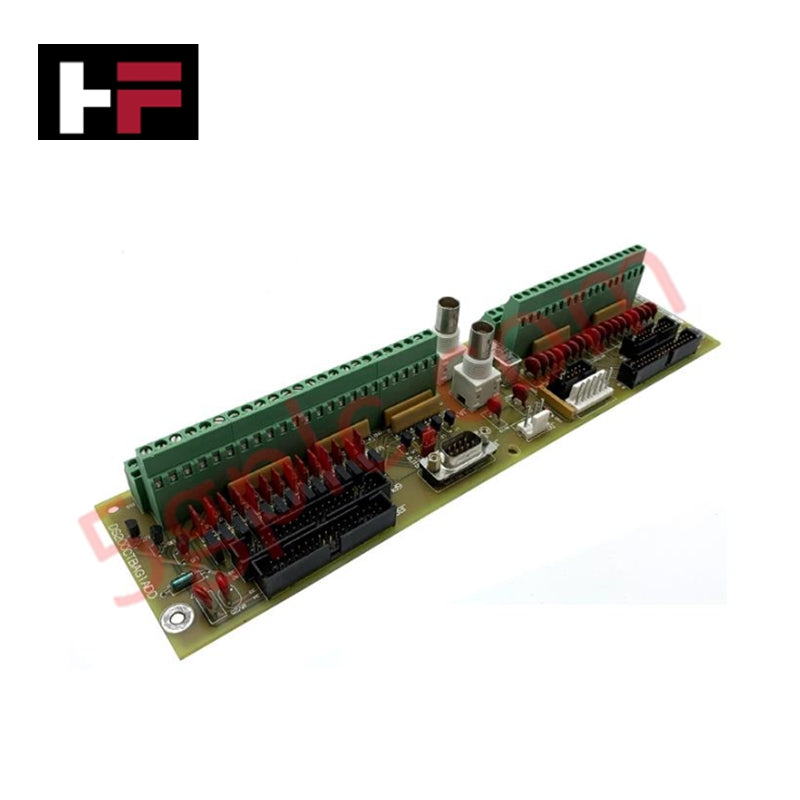
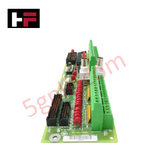
Product Details
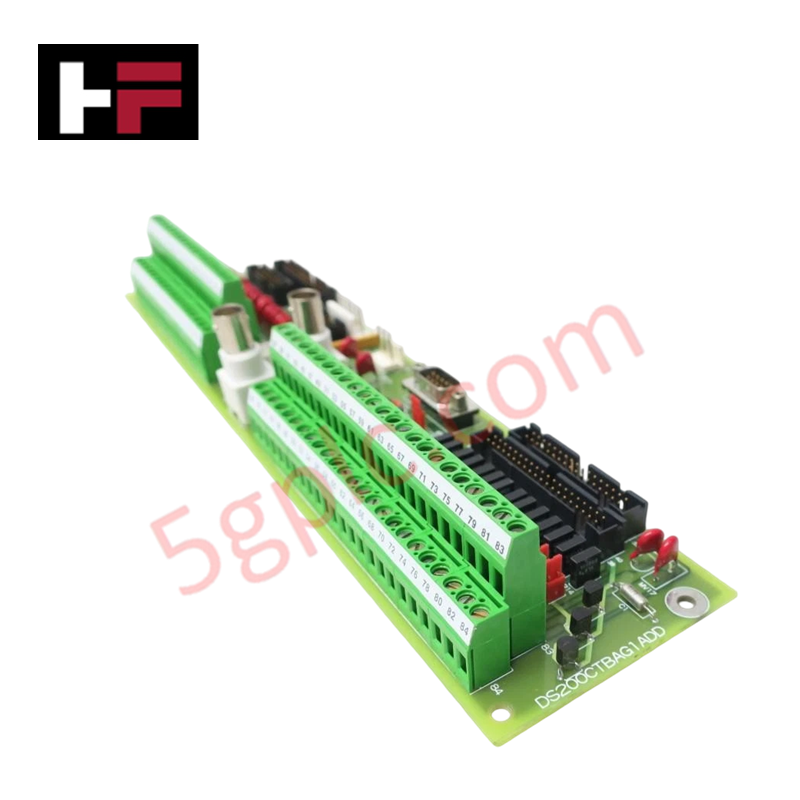
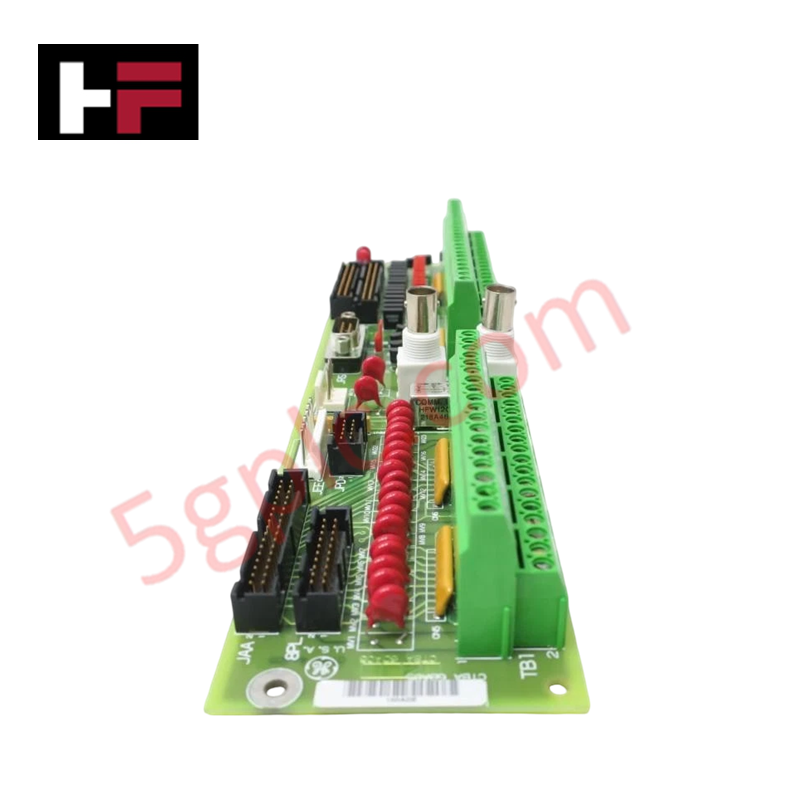
Configured for signal termination and bus communication in Mark V LM control systems, the GE DS200CTBAG1A (DS200CTBA Terminal Board) provides direct physical execution of analog signal routing and core power monitoring.
Hardware Specifications
| Parameter | Specification |
|---|---|
| Model | DS200CTBAG1A |
| Brand | General Electric |
| Origin | USA |
| Dimensions | 6.25 in x 4.25 in |
| Operating Temp | -28 deg C to 55 deg C |
| Core Compatibility | R5 core housing |
| I/O Capabilities | Shaft voltage/current, 4-20 mA input/output |
Backplane Bus Communication and Deterministic Processing
The DS200CTBAG1A facilitates deterministic communication across Mark V LM platforms through integrated IONET and COREBUS interfaces. The board manages connectivity between the R5 core and the STCA/QTBA modules, ensuring signal integrity for 4-20 mA loops and shaft-specific instrumentation. In the event of a localized power loss on the CTBA module, an onboard bypass relay maintains COREBUS communication, preventing system-wide disruption. Connectivity with the PD core's TCPD board allows for continuous power source monitoring. Firmware flash compatibility is not supported; system integration is managed through hardware-defined signal paths and dedicated terminal wiring.
Frequently Asked Questions
Q: What is the function of the onboard bypass relay during a power failure?
A: The bypass relay is configured to maintain COREBUS communication continuity if the CTBA module experiences a loss of power. This allows other modules on the bus to continue data exchange without interruption.
Q: Can the 4-20 mA inputs be scaled via software?
A: No. The CTBA board acts as a passive termination point. Scaling of 4-20 mA signals must be performed within the higher-level controller logic of the connected STCA or R5 core processors.
Field Installation Guidelines
- Ensure the Mark V LM rack is fully de-energized before mounting the module to prevent damage to the backplane connectors or unintended shorting of 4-20 mA loops.
- Verify all field wiring for shaft instrumentation and 4-20 mA signals, ensuring proper shielding is terminated to the designated ground lug to minimize noise.
- Handle the board by the edges to avoid electrostatic discharge (ESD) exposure to the bypass relay and bus communication circuitry.
- After installation, confirm that the IONET and COREBUS link LEDs (if present on associated modules) indicate successful synchronization with the STCA and QTBA boards.
Additional Information
- 100% Genuine Parts: All products are original and authentic, ensuring reliable industrial performance.
- 30-Day Refund Guarantee: Return any in-stock item within 30 days in original, unopened packaging for a full refund (excluding shipping and fees).
- 12-Month Warranty: Covers defects in materials or workmanship; excludes misuse, normal wear, or unauthorized modifications.
- Worldwide Shipping: We ship via USPS, UPS, FedEx, and DHL. Delivery times vary by country and may be subject to customs or import fees.
- Support & Contact: Technical and warranty assistance is available anytime. Contact us here: Contact.
- Purchase Guidance: Check product specifications and compatibility carefully before ordering to ensure proper application.


Tech & Buying Guide

Mastering the Siemens PLC Scan Cycle: How the CPU Executes Automation Programs
Industrial automation relies heavily on programmable logic controllers (PLCs) to manage complex manufacturing processes. Many engineers dive straight into programming without mastering the underlying architecture. However, understanding how a PLC CPU executes a program ensures reliable system design. Therefore, mastering the scan cycle optimizes both performance and troubleshooting in modern control systems.
How to Connect to Siemens S7 PLCs: 5 Essential Communication Methods
Establishing a reliable hardware link between a programming terminal and a Siemens SIMATIC controller is essential for engineering workflows. Field engineers rely on distinct physical layers, ranging from legacy serial connections to high-speed Industrial Ethernet protocols. Modern factory automation environments prioritize fast data transfer and seamless driver integration. Selecting the correct connection method simplifies program downloads, online monitoring, and system troubleshooting in complex control systems.
Will PLCs Become Obsolete? The Future of Control Systems in Industry 4.0
Modern manufacturing is undergoing a rapid technological transformation driven by Industry 4.0 innovations. Technologies like Artificial Intelligence (AI), Machine Learning (ML), and the Industrial Internet of Things (IIoT) are dominating discussions across the factory automation sector. Consequently, many engineers wonder if these advanced digital tools will eventually replace traditional Programmable Logic Controllers (PLCs). However, evaluating the core physics of industrial operations reveals a very different reality for control systems.