










Product Details
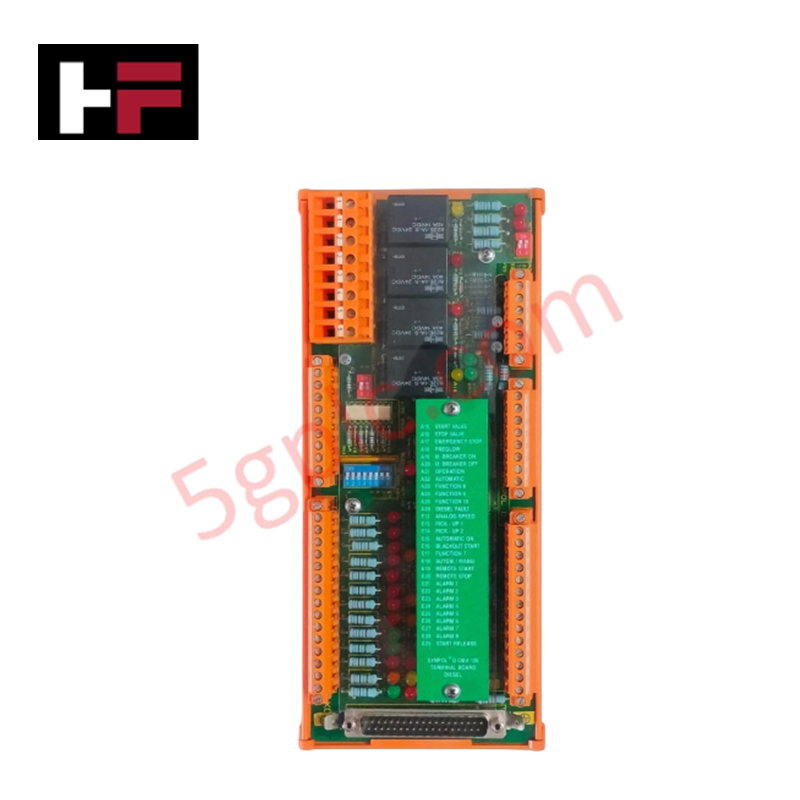
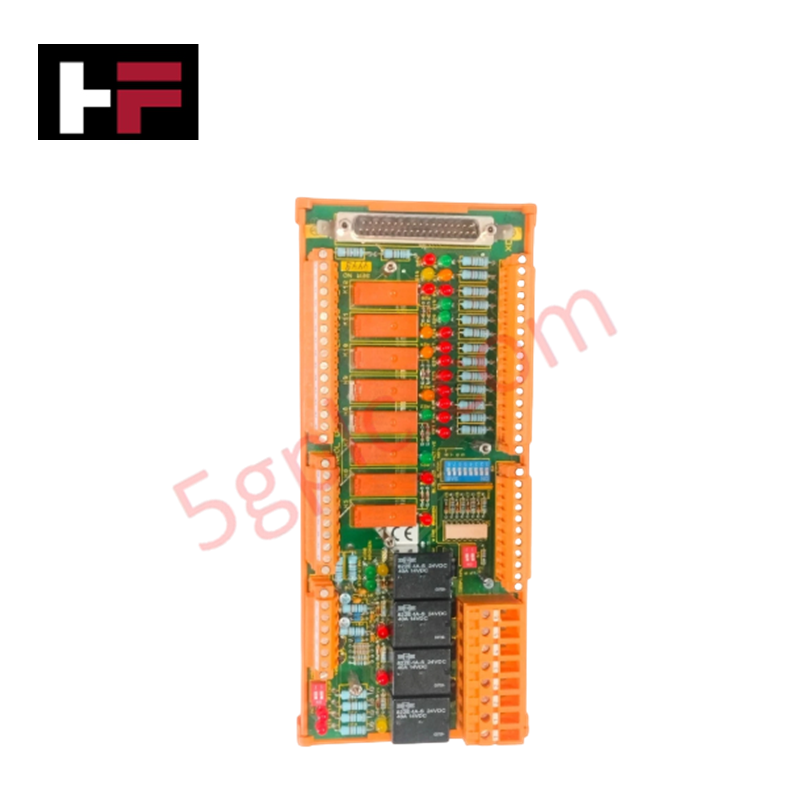
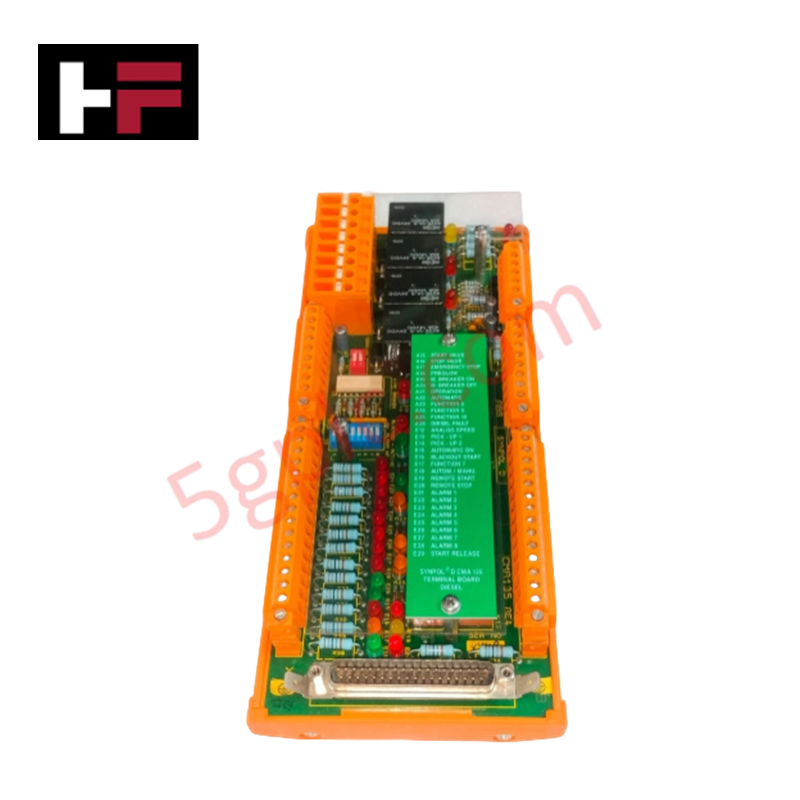
The ABB CMA135 3DDE 300 415, also cataloged as the CMA135 Synpol D Module, operates as a dedicated hardware component for high-density HART signal multiplexing and field device integration within ABB S800 I/O systems.
Hardware Specifications
| Parameter | Specification |
|---|---|
| Model | CMA135 (3DDE 300 415) |
| Brand | ABB |
| Origin | Sweden |
| Weight | 0.7 kg |
| Dimensions | 45 mm x 100 mm x 125 mm |
| Operating Temp | -25 to +70 deg C |
| Power Consumption | ~2.5 W (24 VDC via S800 I/O baseplate) |
| HART Channels | 16 channels (multiplexed, HART 5, 6, 7 all revisions) |
| Isolation | 1500 VAC (channel-to-channel and channel-to-system) |
| Communication Interface | ABB internal S800 bus |
| Field Interface | 2 x M12 connectors (8 HART pairs each) |
| Relative Humidity | 5% to 95% (non-condensing) |
Backplane Bus Communication Velocity and Firmware Flash Compatibility
The CMA135 module processes multiplexed HART variable polling without degrading backplane bus communication velocity across the host S800 I/O backplane. Hardware-level 1500 VAC channel isolation protects internal signal processing circuits from earth potential shifts and field-induced noise. Standardized firmware flash compatibility across ABB controller platforms ensures deterministic data updates and seamless I/O density scaling across distributed node configurations.
Frequently Asked Questions
Q: How is primary operating power supplied to the CMA135 module?
A: Power is drawn directly from the 24 VDC auxiliary bus embedded within the S800 I/O baseplate, consuming approximately 2.5 W during standard operation.
Q: What isolation rating exists between individual HART channels and the system logic?
A: Galvanic isolation rated at 1500 VAC is maintained channel-to-channel as well as between individual channels and the backplane logic interface.
Q: Are field connection points wired via standard terminal blocks or specialized connectors?
A: Signal wiring connects through two M12 field connectors, with each M12 interface accepting 8 twisted HART channel pairs.
Field Installation Guidelines
- Turn off 24 VDC baseplate power and verify system isolation prior to seating the CMA135 module.
- Wear an ESD wrist strap connected to cabinet frame earth ground during board handling.
- Align the module housing guide pins with the target slot on the S800 baseplate and push firmly until fully latched.
- Secure M12 field connector plugs onto the front panel receptacles, tightening retaining collars to ensure solid contact and IP-rated sealing.
- Apply power to the S800 baseplate and verify module boot status and HART channel communication LEDs via controller diagnostic software.
Additional Information
- 100% Genuine Parts: All products are original and authentic, ensuring reliable industrial performance.
- 30-Day Refund Guarantee: Return any in-stock item within 30 days in original, unopened packaging for a full refund (excluding shipping and fees).
- 12-Month Warranty: Covers defects in materials or workmanship; excludes misuse, normal wear, or unauthorized modifications.
- Worldwide Shipping: We ship via USPS, UPS, FedEx, and DHL. Delivery times vary by country and may be subject to customs or import fees.
- Support & Contact: Technical and warranty assistance is available anytime. Contact us here: Contact.
- Purchase Guidance: Check product specifications and compatibility carefully before ordering to ensure proper application.
Tech & Buying Guide

Why Programmable Logic Controllers Drop into Stop Mode: An Expert Analysis
Industrial automation systems rely heavily on Programmable Logic Controllers (PLCs) to maintain uninterrupted production. When a PLC unexpectedly shifts from Run to Stop mode, whole manufacturing lines stall.
As control systems evolve across modern factory automation, understanding the root causes of these interruptions helps engineers minimize costly downtime. This technical guide breaks down why PLCs trip into Stop mode and provides practical strategies to mitigate system faults.

Understanding Root Causes of Unplanned PLC Stop Mode in Industrial Automation
Modern Programmable Logic Controllers manage execution through distinct operational states: Run, Stop, Start-Up, and Hold. During power-up, a controller initializes memory registers within Stop mode before briefly transitioning to Start-Up mode. During this phase, internal self-diagnostics evaluate system integrity across hardware and user programs. If the controller detects no critical faults, it enters Run mode to execute the control program continuously. However, any severe system anomaly forces the CPU back into Stop mode immediately to prevent erratic machine behavior across the plant floor.

Human-Machine Interface Design: Essential Guide to HMI Selection, Visualization, and Control System Integration
Human-Machine Interfaces (HMIs) serve as the primary operational window into complex industrial automation systems. Modern HMIs convert raw machine data into clear graphical displays, enabling operators to oversee entire manufacturing processes in real time. Instead of relying on physical control panels full of hardwired switches, engineers program interactive screens using intuitive graphics, dynamic color coding, and responsive touch interfaces. Over my 15 years in control systems engineering, I have observed HMIs transform from basic display screens into sophisticated command centers that drive operational efficiency across DCS and PLC environments.