










Product Details
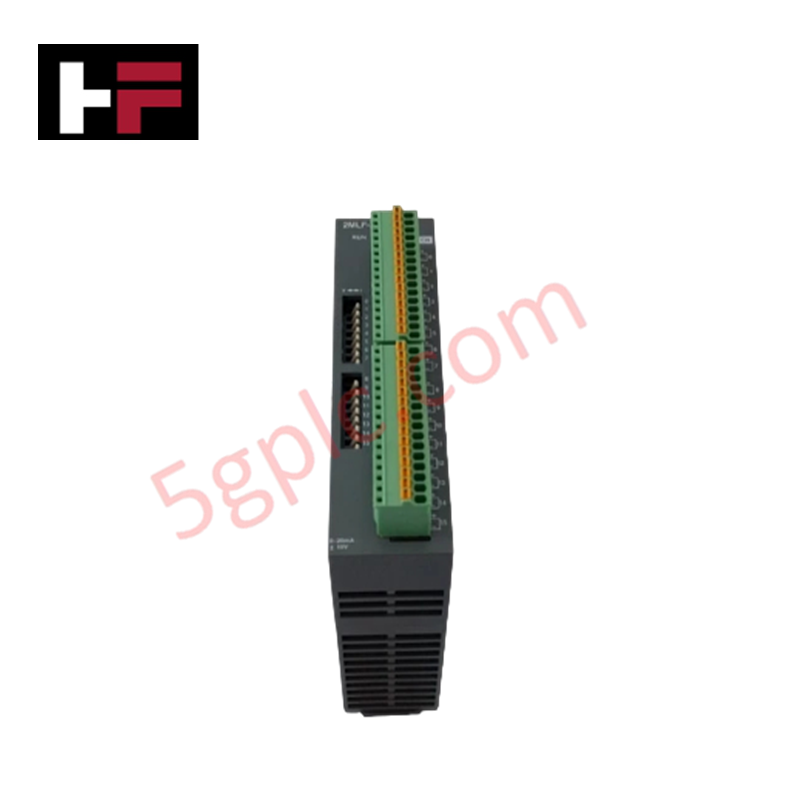
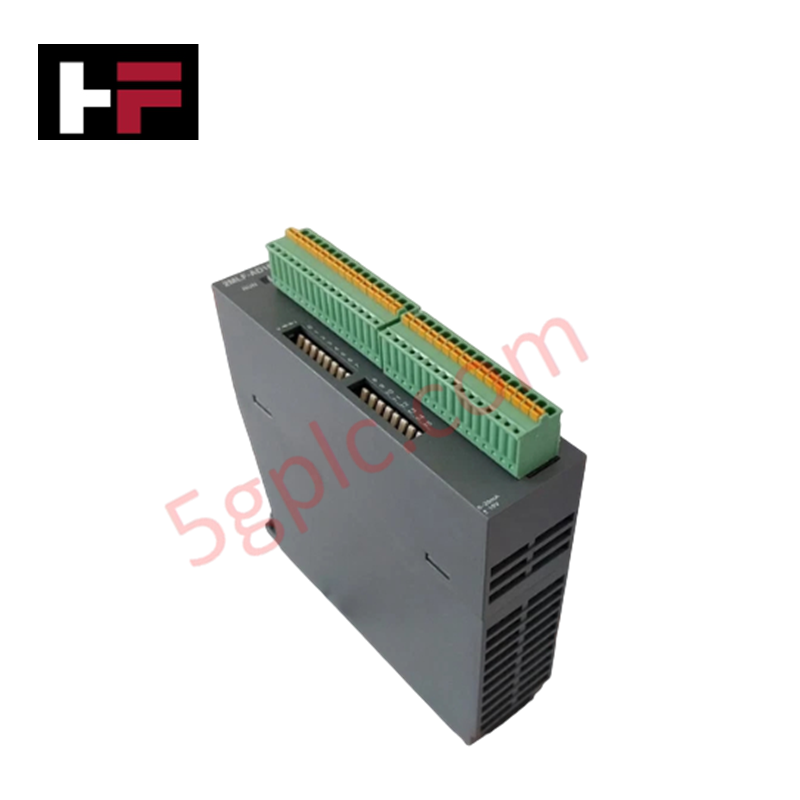
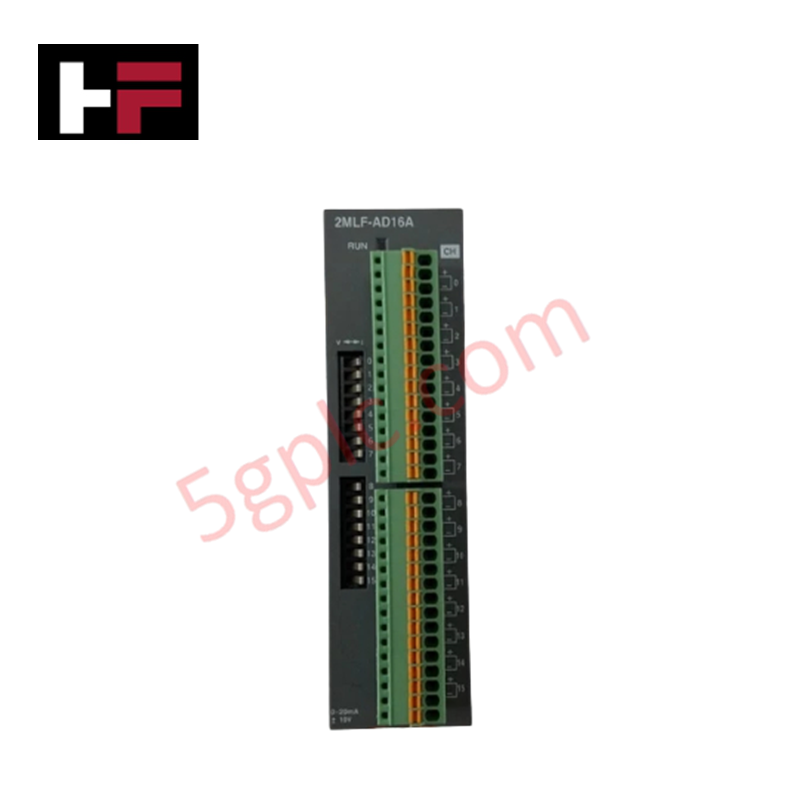
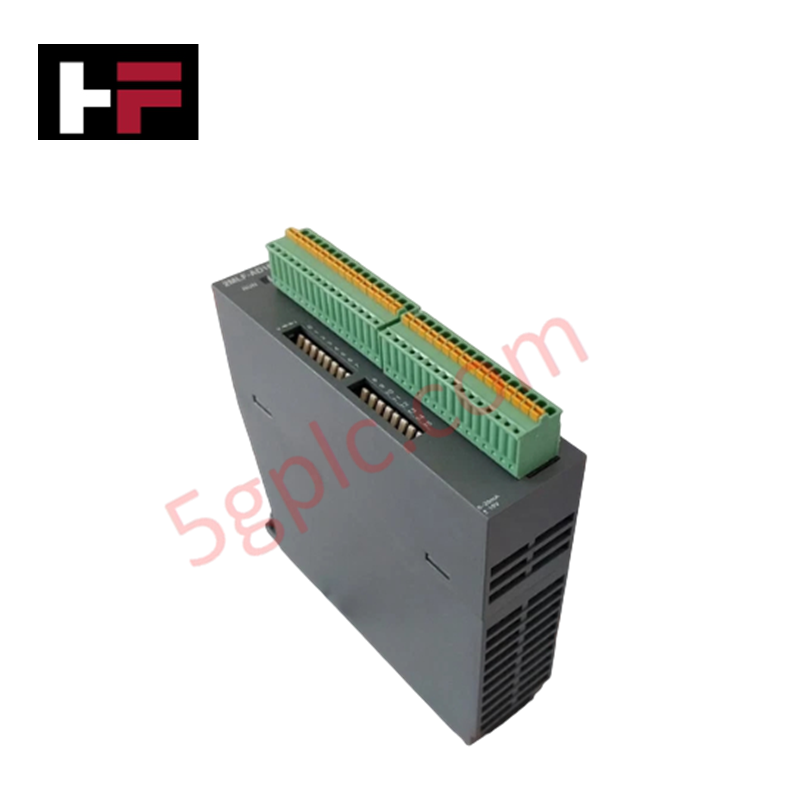
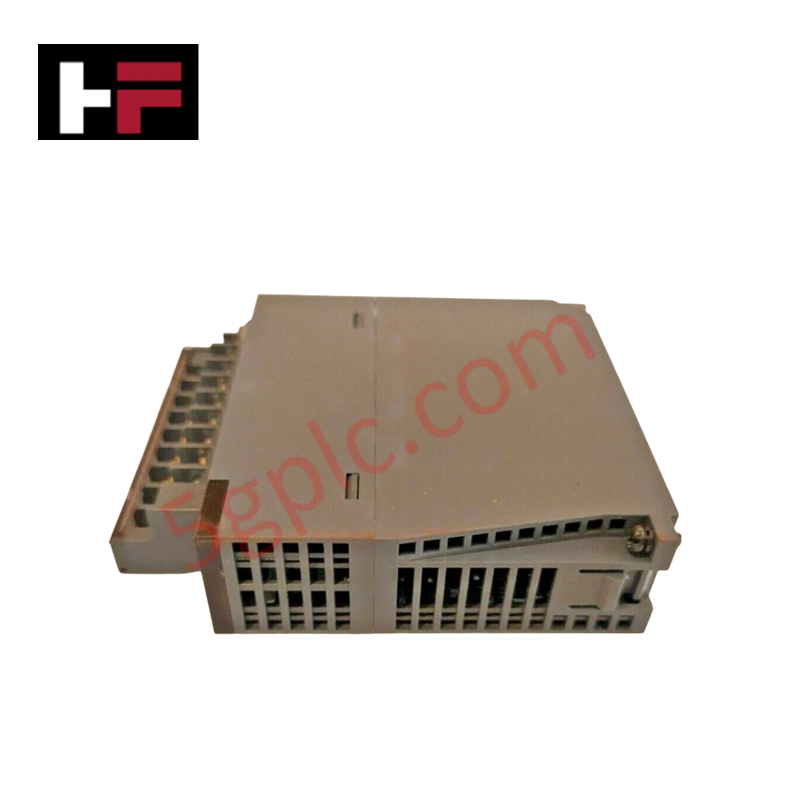
Configured for multi-channel voltage/current signal acquisition in MasterLogic-200 PLC networks, the Honeywell 2MLF-AD16A-CC (2MLF-AD16A-CC Analog Input Module) provides direct physical/electrical execution.
Hardware Specifications
| Parameter | Specification |
|---|---|
| Model | 2MLF-AD16A-CC |
| Brand | Honeywell |
| Origin | South Korea |
| Weight | 0.115 kg |
| Dimensions | Standard MasterLogic-200 I/O Module Form Factor |
| Operating Temp | 0 to 55 deg C |
| Power Consumption | 330 mA at 5 VDC (internal backplane) |
| Input Channels | 16 channels |
| Max Conversion Speed | 500 us / channel |
| Accuracy | +/-0.2% (at 25 +/-5 deg C), +/-0.3% (at 0 to 55 deg C) |
| Isolation Method | Photo-coupler between input and PLC power (non-isolated channel-to-channel) |
| Terminal Connection | 32-point terminal block |
| Assigned I/O Addresses | Fixed type: 64 points; Variable type: 16 points |
| Storage Temp | -25 to +70 deg C |
| Operating Humidity | 5% to 95% RH (non-condensing) |
Process Control Signal Conditioning and Loop Protocol
The 2MLF-AD16A-CC executes high-speed analog-to-digital conversion across 16 field input channels using a photo-coupler isolation barrier rated between the field wiring terminals and the backplane logic power supply. Designed to process 4-20 mA HART loop protocol transmitters and standard analog instrumentation, the module maintains an absolute conversion rate of 500 us per channel while filtering common-mode field noise. Thermal drift compensation algorithms retain signal conversion precision within +/-0.2% under nominal operating conditions.
Frequently Asked Questions
Q: Does the 2MLF-AD16A-CC feature channel-to-channel galvanic isolation?
A: No, the module provides photo-coupler isolation between the field input terminals and the internal PLC backplane power, but does not provide individual isolation between input channels.
Q: How many I/O points are allocated on the backplane bus for the 2MLF-AD16A-CC?
A: The module assigns either 64 fixed points or 16 variable points depending on the configured addressing mode within the MasterLogic-200 system environment.
Field Installation Guidelines
- Power off the main backplane chassis prior to seating the 2MLF-AD16A-CC module into the MasterLogic-200 rack slot.
- Align the module housing with the base guide rails and press firmly until the upper and lower mounting latches lock securely.
- Wire field analog instrumentation to the 32-point terminal block using shielded twisted-pair cabling.
- Ground cable shields at a single ground busbar inside the cabinet to prevent stray ground loop currents from affecting measurement accuracy across non-isolated channels.
Additional Information
- 100% Genuine Parts: All products are original and authentic, ensuring reliable industrial performance.
- 30-Day Refund Guarantee: Return any in-stock item within 30 days in original, unopened packaging for a full refund (excluding shipping and fees).
- 12-Month Warranty: Covers defects in materials or workmanship; excludes misuse, normal wear, or unauthorized modifications.
- Worldwide Shipping: We ship via USPS, UPS, FedEx, and DHL. Delivery times vary by country and may be subject to customs or import fees.
- Support & Contact: Technical and warranty assistance is available anytime. Contact us here: Contact.
- Purchase Guidance: Check product specifications and compatibility carefully before ordering to ensure proper application.






Tech & Buying Guide

FAT vs SAT in Industrial Control Systems: Key Differences and Execution Guide
Industrial control system deployment relies on strict verification protocols to guarantee operational safety, system stability, and regulatory compliance. Commissioning complex Programmable Logic Controller (PLC) racks, Distributed Control Systems (DCS), and Safety Instrumented Systems (SIS) requires two critical milestones: the Factory Acceptance Test (FAT) and the Site Acceptance Test (SAT). Both procedures validate that system automation meets design specifications, but they occur at different stages of project execution and target distinct operational risks.

Hub vs Switch vs Router in Industrial Automation Architecture
Modern factory automation relies on reliable industrial networking infrastructure to exchange real-time field data across operational technology systems. Engineers often encounter networking hardware like hubs, switches, and routers when integrating Programmable Logic Controllers, Distributed Control Systems, and SCADA monitoring nodes. Although these devices share physical ports, they operate at different layers of the Open Systems Interconnection reference model and deliver distinct traffic management capabilities.

Marshalling Cabinet Preventive Maintenance: Essential Healthiness Checks for PLC, DCS, and ESD Systems
Marshalling cabinets serve as the vital interface between field instrumentation and control room electronics in modern process facilities. Regular preventive maintenance of these cabinets ensures signal integrity across programmable logic controllers (PLCs), distributed control systems (DCS), and emergency shutdown (ESD) networks. System technicians must execute structured inspection protocols to mitigate environmental risks, identify loose wiring, and maintain continuous operational readiness.