












Product Details
Overview
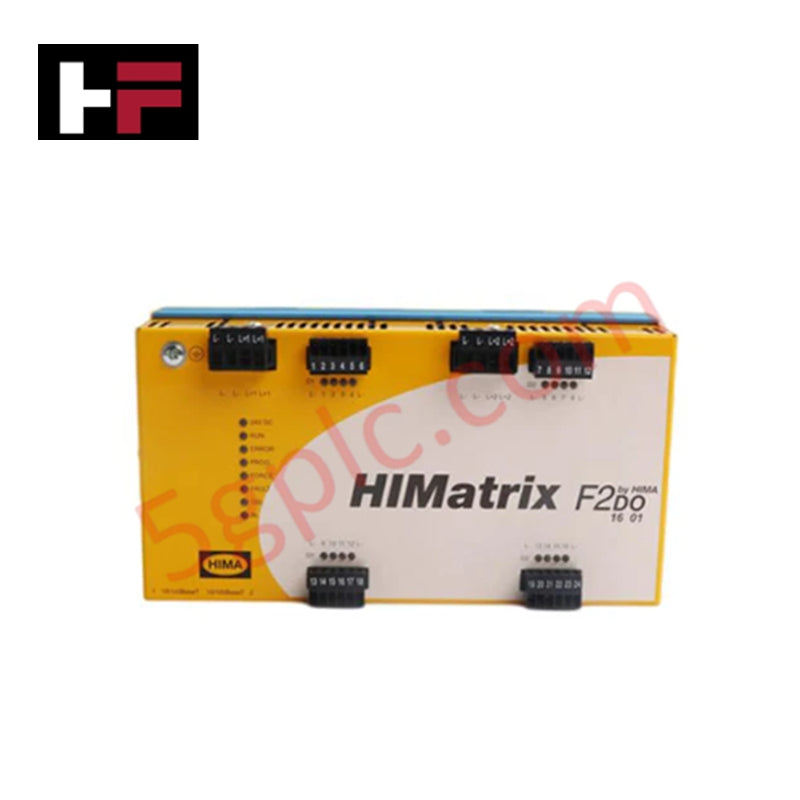
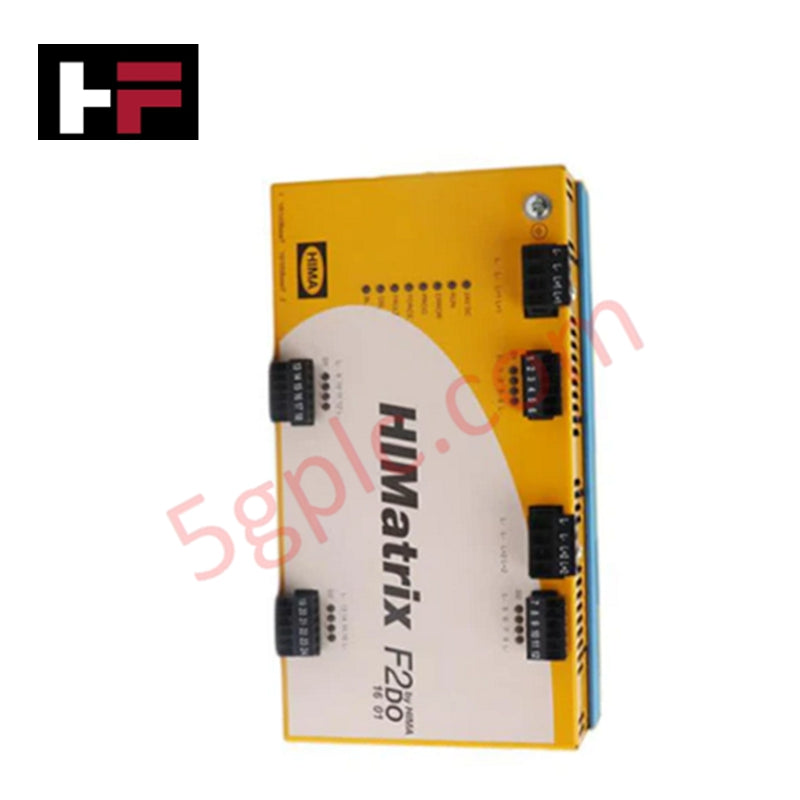
The HIMA F2 DO 16 02/F2DO1602 is a safety-related remote output module engineered for high availability and robust performance in critical industrial automation systems. It is part of the HIMatrix F2 series and provides reliable SIL 3 performance for diverse safety applications. Designed for compact installation, this module supports streamlined communication and easy integration into existing control networks.
Technical Specifications
-
Manufacturer: HIMA
-
Model Number: F2 DO 16 02/F2DO1602
-
Product Type: Safety Controller Remote Output Module
-
Safety Integrity Level (SIL): 3
-
Number of Digital Inputs: 16
-
Number of Digital Outputs: 16
-
Communication Protocol: Modbus TCP/IP
-
Mounting: DIN rail
-
Dimensions (L × W × H): 25.3 × 11.6 × 10 cm
-
Weight: 2 kg
-
Key Features: Compact form factor, high availability, and wide safety application coverage
Key Features
-
Certified SIL 3 for maximum safety compliance
-
Supports 16 digital inputs and 16 digital outputs
-
Modbus TCP/IP communication for network integration
-
Compact DIN rail mounting for flexible installation
-
Designed for high reliability and continuous operation
Application Scenarios
The HIMA F2 DO 16 02 is suitable for:
-
Safety interlock and emergency shutdown systems
-
Process automation requiring remote output monitoring
-
Integration into HIMatrix F2 series safety networks
-
Industrial facilities demanding high system uptime and reliability
FAQ
Q: What safety standard does the F2DO1602 meet?
A: The module is SIL 3 certified, ensuring compliance with IEC 61508 safety standards.
Q: Can it communicate with existing Modbus networks?
A: Yes. The F2DO1602 supports Modbus TCP/IP for seamless integration into existing networks.
Q: What installation options are available?
A: It is designed for DIN rail mounting in standard control panels.
Additional Information
- 100% Genuine Parts: All products are original and authentic, ensuring reliable industrial performance.
- 30-Day Refund Guarantee: Return any in-stock item within 30 days in original, unopened packaging for a full refund (excluding shipping and fees).
- 12-Month Warranty: Covers defects in materials or workmanship; excludes misuse, normal wear, or unauthorized modifications.
- Worldwide Shipping: We ship via USPS, UPS, FedEx, and DHL. Delivery times vary by country and may be subject to customs or import fees.
- Support & Contact: Technical and warranty assistance is available anytime. Contact us here: Contact.
- Purchase Guidance: Check product specifications and compatibility carefully before ordering to ensure proper application.




Tech & Buying Guide

Why Programmable Logic Controllers Drop into Stop Mode: An Expert Analysis
Industrial automation systems rely heavily on Programmable Logic Controllers (PLCs) to maintain uninterrupted production. When a PLC unexpectedly shifts from Run to Stop mode, whole manufacturing lines stall.
As control systems evolve across modern factory automation, understanding the root causes of these interruptions helps engineers minimize costly downtime. This technical guide breaks down why PLCs trip into Stop mode and provides practical strategies to mitigate system faults.

Understanding Root Causes of Unplanned PLC Stop Mode in Industrial Automation
Modern Programmable Logic Controllers manage execution through distinct operational states: Run, Stop, Start-Up, and Hold. During power-up, a controller initializes memory registers within Stop mode before briefly transitioning to Start-Up mode. During this phase, internal self-diagnostics evaluate system integrity across hardware and user programs. If the controller detects no critical faults, it enters Run mode to execute the control program continuously. However, any severe system anomaly forces the CPU back into Stop mode immediately to prevent erratic machine behavior across the plant floor.

Human-Machine Interface Design: Essential Guide to HMI Selection, Visualization, and Control System Integration
Human-Machine Interfaces (HMIs) serve as the primary operational window into complex industrial automation systems. Modern HMIs convert raw machine data into clear graphical displays, enabling operators to oversee entire manufacturing processes in real time. Instead of relying on physical control panels full of hardwired switches, engineers program interactive screens using intuitive graphics, dynamic color coding, and responsive touch interfaces. Over my 15 years in control systems engineering, I have observed HMIs transform from basic display screens into sophisticated command centers that drive operational efficiency across DCS and PLC environments.