










Product Details
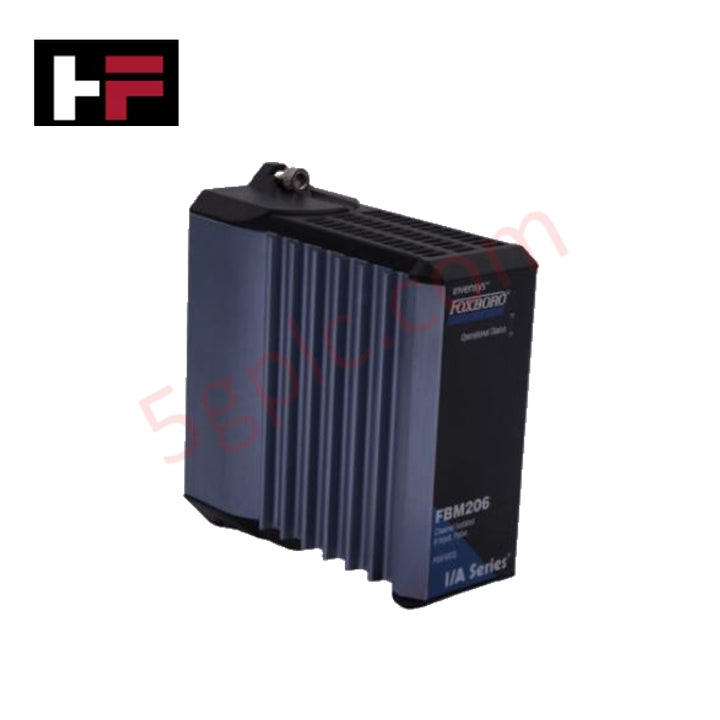
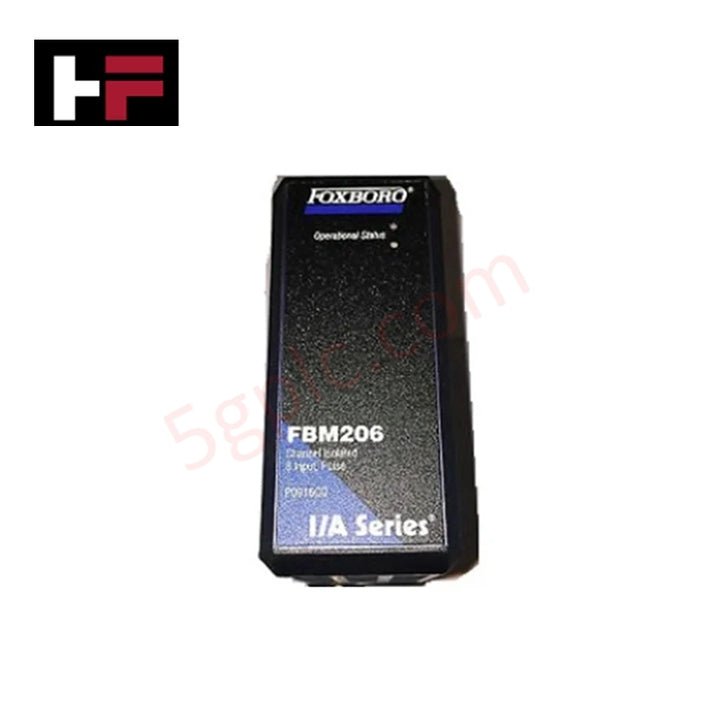
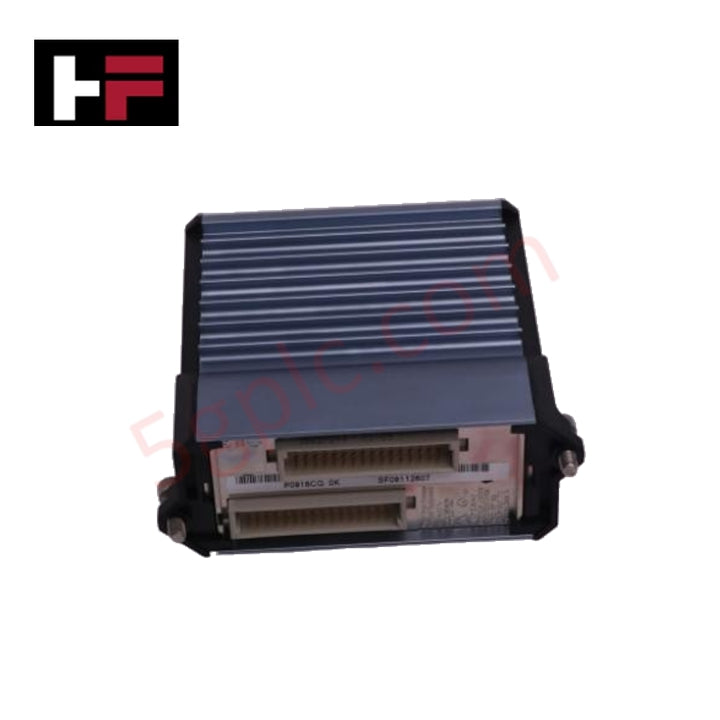
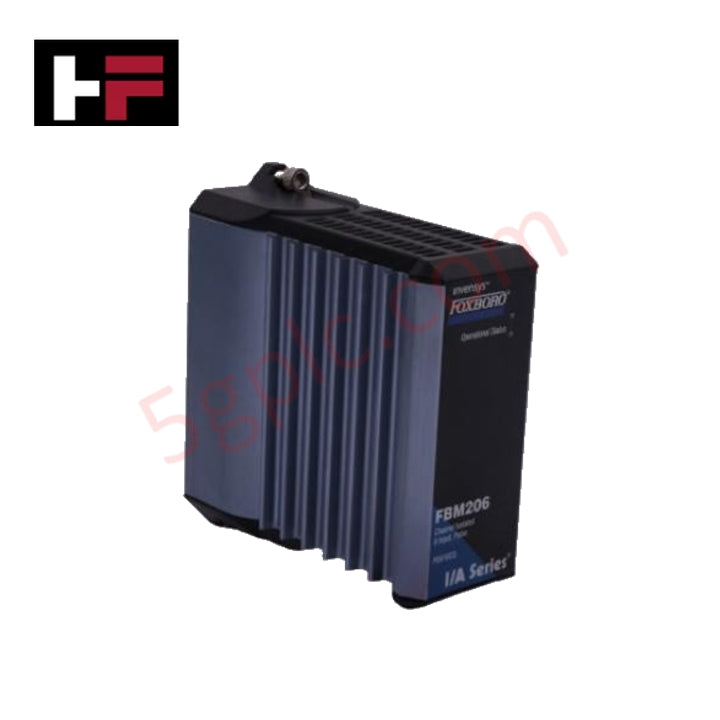
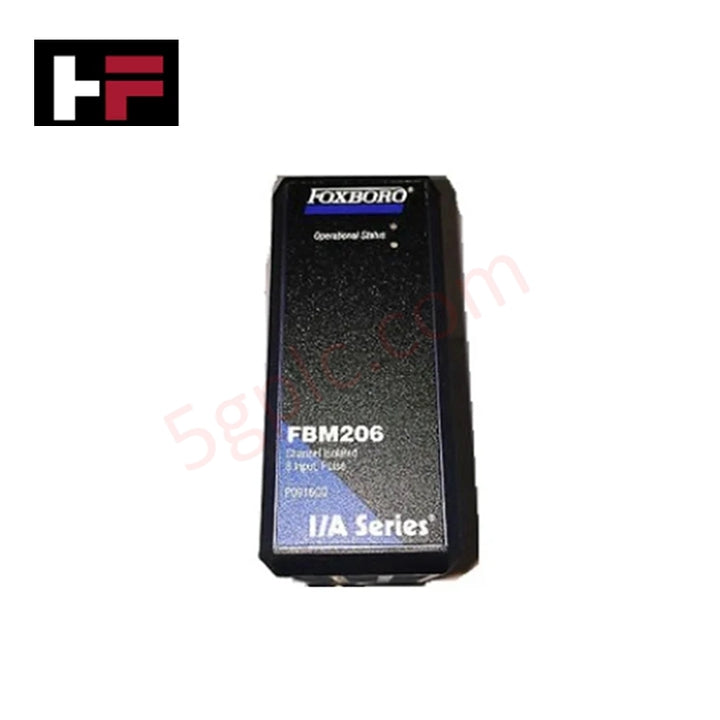
Foxboro FBM206 I/A Series Pulse Input Fieldbus Module
The Foxboro FBM206, also cataloged as the FBM206 Pulse Input Fieldbus Module, operates as a dedicated hardware component for high-speed signal processing within Foxboro I/A Series and Foxboro Evo DCS platforms. The module accepts up to eight independent pulse input channels from field transmitters, including turbine flowmeters, vortex flowmeters, and rotational speed sensors. Communicating across a redundant 2 Mbps Module Fieldbus, the board converts incoming 7 to 27 VDC pulse trains into digital data for precise rate measurement and totalization.
Hardware Specifications
| Parameter | Specification |
|---|---|
| Model | FBM206 |
| Brand | Foxboro / Schneider Electric |
| Origin | USA |
| Weight | 0.32 kg |
| Dimensions | 4.5 cm x 11 cm x 11.5 cm |
| Operating Temp | -20 to +70 deg C |
| Power Consumption | 24 VDC nominal (Field device supply: 30 mA max per channel) |
| Input Channels | 8 Pulse / Frequency Input Channels |
| Maximum Pulse Rate | 25 kHz (10 Hz to 25 kHz specified range) |
| Pulse Rate Accuracy | 0.01% of reading |
| Channel Isolation | Galvanically isolated channel-to-channel and channel-to-ground (600 VAC for 1 min) |
| System Platform | Foxboro I/A Series / Foxboro Evo DCS |
Process Control and Digital Interface
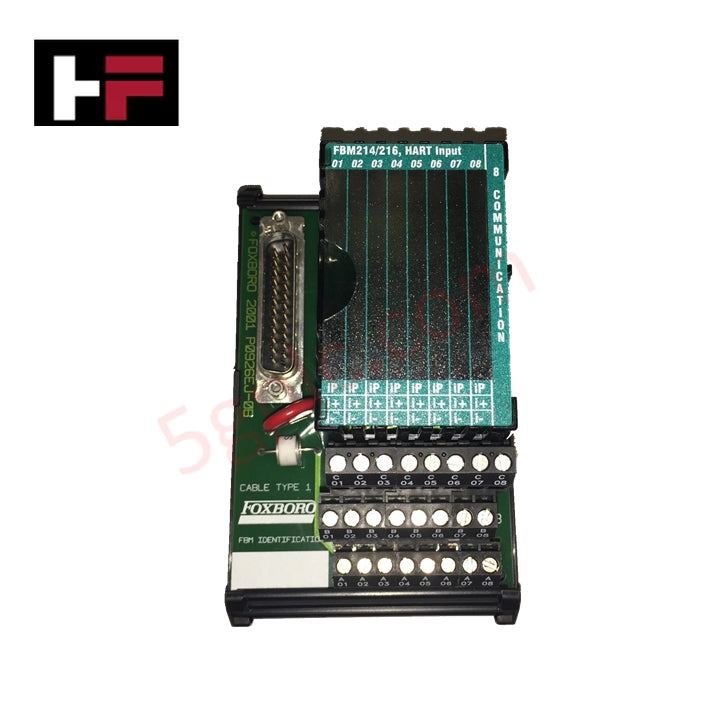
Each input channel features dedicated galvanic isolation to prevent cross-talk and eliminate ground loop interference between field sensors and the central processor backplane. Supporting 4-20 mA HART loop protocol routing alongside discrete digital frequency lines in shared termination cabinets, the module incorporates robust signal-conditioning circuits that maintain totalization accuracy without missing pulses across its full 10 Hz to 25 kHz range. Onboard microprocessor logic handles individual meter scaling and totalization parameters before transmitting process data over the redundant 2 Mbps Fieldbus.
Frequently Asked Questions
Q: How does the module handle power distribution to connected field sensors?
A: The module provides an integral 24 VDC field device supply delivering up to 30 mA per channel to power external solid-state sensors, vortex transmitters, or pulse transducers directly.
Q: What mechanisms prevent signal loss during high-frequency pulse acquisition?
A: Integrated hardware counters and galvanic optocouplers maintain pulse count integrity up to 25 kHz, delivering an accuracy of 0.01% of reading with zero missed pulses within the 10 Hz to 25 kHz operating band.
Q: Can the module be replaced while the system is powered?
A: Yes, the modular chassis design supports hot-swapping into standard Foxboro baseplates, allowing technicians to replace the unit without disrupting communication on the redundant Module Fieldbus.
Field Installation Guidelines
Align the module housing with the designated slot on the Foxboro I/A Series baseplate and push firmly until the locking mechanisms engage. Secure all baseplate mounting hardware to ensure continuous contact with the backplane bus. Connect a 14 AWG earth ground wire from the baseplate grounding stud directly to the main cabinet ground bar to maintain an effective low-impedance path for transient surge suppression.
Route incoming pulse signal lines through DIN-rail mounted Termination Assemblies (TA), maintaining terminal connections using twisted-pair shielded cabling up to a maximum length of 30 m. Ground all cable shields at a single chassis ground point to prevent ambient electrical noise from interfering with high-speed pulse detection. Technicians must wear a grounded ESD wrist strap whenever handling unmounted modules or adjusting field wiring termination connections.
Additional Information
- 100% Genuine Parts: All products are original and authentic, ensuring reliable industrial performance.
- 30-Day Refund Guarantee: Return any in-stock item within 30 days in original, unopened packaging for a full refund (excluding shipping and fees).
- 12-Month Warranty: Covers defects in materials or workmanship; excludes misuse, normal wear, or unauthorized modifications.
- Worldwide Shipping: We ship via USPS, UPS, FedEx, and DHL. Delivery times vary by country and may be subject to customs or import fees.
- Support & Contact: Technical and warranty assistance is available anytime. Contact us here: Contact.
- Purchase Guidance: Check product specifications and compatibility carefully before ordering to ensure proper application.
Tech & Buying Guide

Why Programmable Logic Controllers Drop into Stop Mode: An Expert Analysis
Industrial automation systems rely heavily on Programmable Logic Controllers (PLCs) to maintain uninterrupted production. When a PLC unexpectedly shifts from Run to Stop mode, whole manufacturing lines stall.
As control systems evolve across modern factory automation, understanding the root causes of these interruptions helps engineers minimize costly downtime. This technical guide breaks down why PLCs trip into Stop mode and provides practical strategies to mitigate system faults.

Understanding Root Causes of Unplanned PLC Stop Mode in Industrial Automation
Modern Programmable Logic Controllers manage execution through distinct operational states: Run, Stop, Start-Up, and Hold. During power-up, a controller initializes memory registers within Stop mode before briefly transitioning to Start-Up mode. During this phase, internal self-diagnostics evaluate system integrity across hardware and user programs. If the controller detects no critical faults, it enters Run mode to execute the control program continuously. However, any severe system anomaly forces the CPU back into Stop mode immediately to prevent erratic machine behavior across the plant floor.

Human-Machine Interface Design: Essential Guide to HMI Selection, Visualization, and Control System Integration
Human-Machine Interfaces (HMIs) serve as the primary operational window into complex industrial automation systems. Modern HMIs convert raw machine data into clear graphical displays, enabling operators to oversee entire manufacturing processes in real time. Instead of relying on physical control panels full of hardwired switches, engineers program interactive screens using intuitive graphics, dynamic color coding, and responsive touch interfaces. Over my 15 years in control systems engineering, I have observed HMIs transform from basic display screens into sophisticated command centers that drive operational efficiency across DCS and PLC environments.